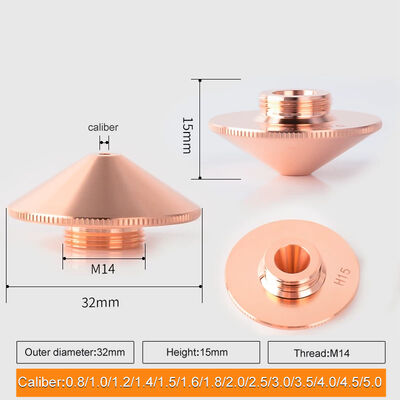
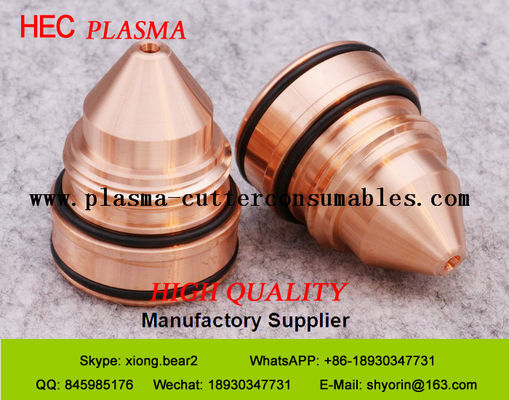
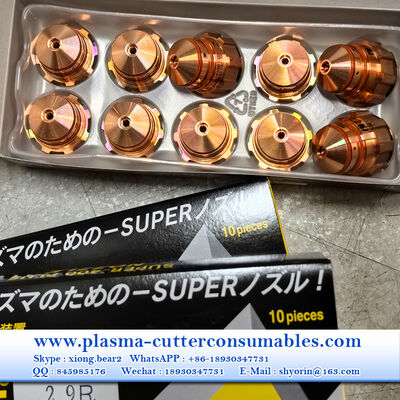
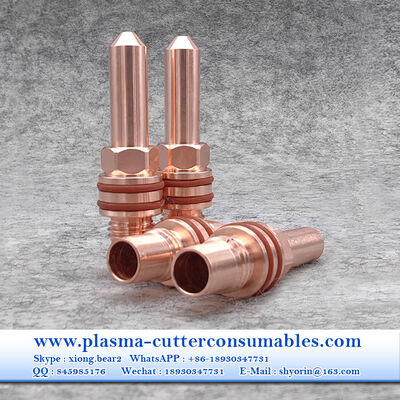
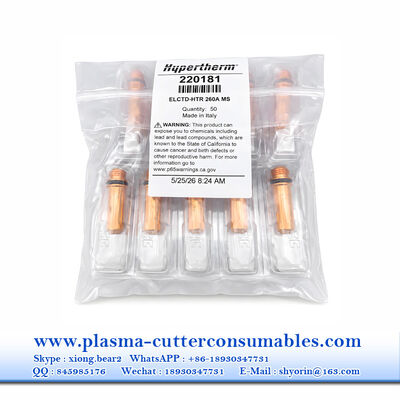
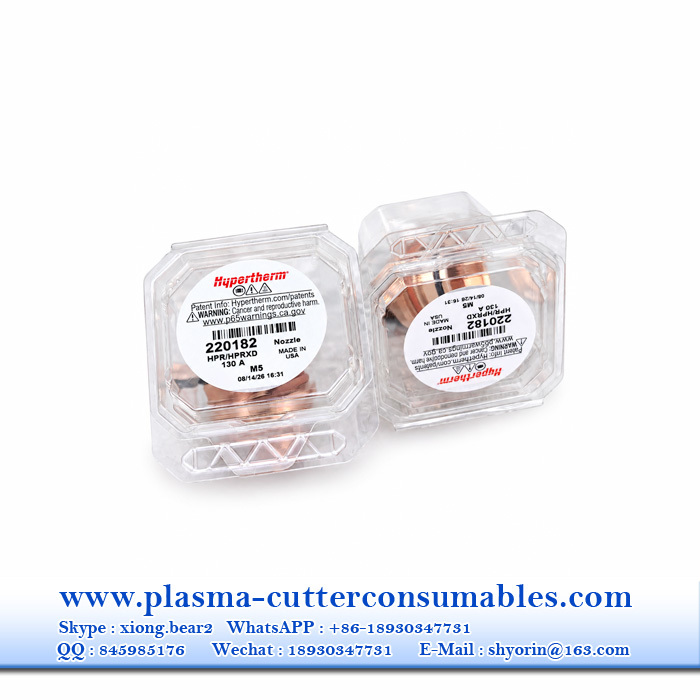
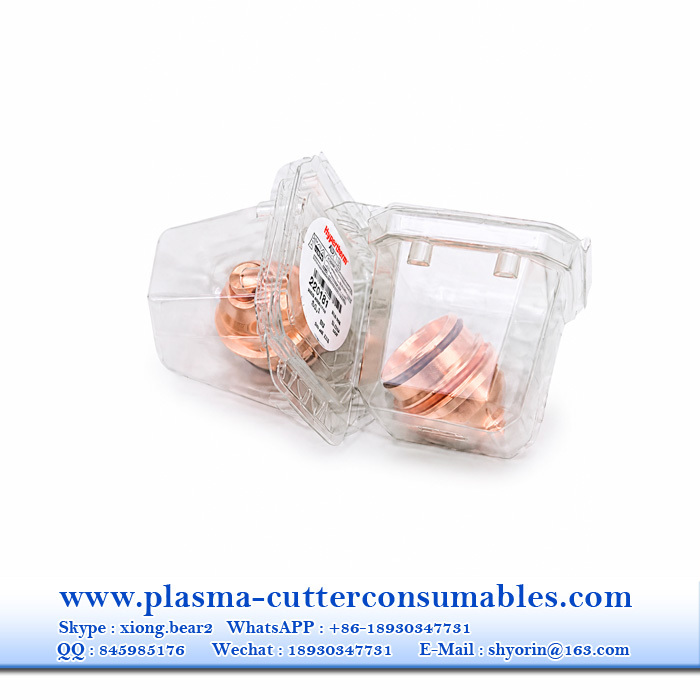
220891 Plasma Nozzle, Oxygen Plasma Cutting Machine Parts
(1) Cutting Current
The cutting current depends on the material and thickness of the workpiece. Higher thickness requires higher cutting current.
(2) Cutting Speed
Cutting speed is determined by material thickness and cutting current. It greatly affects cut quality. Excessively fast speed prevents the plasma arc from fully melting the metal.
(3) Nozzle Stand-off Height
Maintain 2–4 mm clearance between the nozzle tip and the metal workpiece surface.
(4) Working Gas
Oxygen for mild steel cutting. Use clean, dry gas for stable arc and longer consumable service life.
| Machine | HEC NO. | Ref NO. | Description |
|
MAXPRO200 HyPro2000 |
H02487 | 220487 | Electrode,130Amp |
| H02937 | 220937 | Electrode,200Amp | |
| H02925 | 220925 | Electrode-AG,200Amp | |
| H72488 | 220488 | Swirl Ring,Air/Air,130/200Amp | |
| H72834 | 220834 | Swirl Ring,Oxygen/Air, 200Amp | |
| H12892 | 220892 | Nozzle,Air/Air,N2/N2, 130Amp | |
| H12893 | 220893 | Nozzle,Oxygen/Air,130Amp | |
| H12044 | 420044 | Nozzle,Air/Air,N2/N2, 200Amp | |
| H12831 | 220831 | Nozzle,Oxygen/Air,200Amp | |
| H42935 | 220935 | Retaining Cap,50/130/200Amp | |
| H42936 | 220936 | Retaining Cap ,50/130/200Amp | |
| H22536 | 220536 | Shield,Air/Air,N2/N2, 130Amp | |
| H22491 | 220491 | Shield,Oxygen/Air,130Amp | |
| H22045 | 420045 | Shield,Air/Air,N2/N2, 200Amp | |
| H22832 | 220832 | Shield,Oxygen/Air,200Amp | |
| H82087 | 420087 | Torch body | |
| H82033 | 420033 | Quick-Torch body | |
| H82913 | 220913 | Quick-disconnect receptacle | |
| H82921 | 220921 | Quick-Torch body | |
| H92521 | 220521 | Water tube, Standard | |
| H92026 | 044026 | O-Ring |